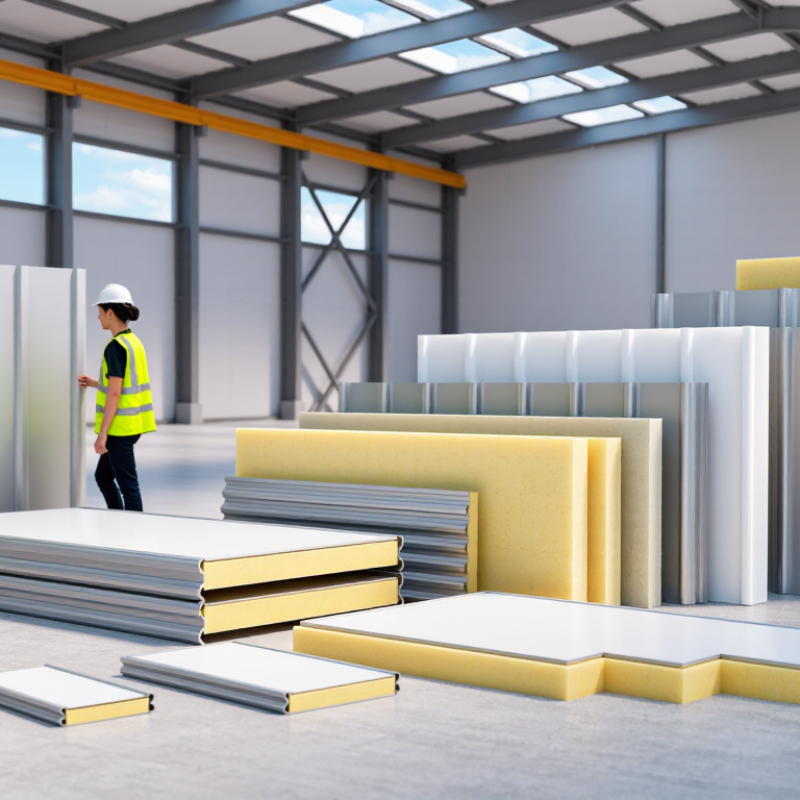
| Panel thickness | Thin, medium, or high-insulation panels | Commonly 40–200 mm; select according to thermal design calculations | Thicker panels improve thermal resistance but increase weight, trim depth, handling space, and fastening requirements. | Use thinner panels for internal partitions and thicker panels for refrigerated or highly insulated envelopes. |
| Panel length | Single-span or multiple shorter panels | Often manufactured to project-specific lengths; transport and lifting limits govern the maximum practical size. | Longer panels reduce horizontal or vertical joints but require more lifting control and sufficient access clearance. | Choose the longest safe panels that can be transported, lifted, and positioned without bending or impact damage. |
| Panel width and module | Standard modular width or project-adjusted width | Common effective widths are approximately 1,000–1,200 mm, subject to the panel system. | The module determines the number of panels, joint locations, cutting requirements, and alignment at openings. | Coordinate the panel module with column spacing, doors, windows, and service penetrations to reduce cutting. |
| Joint type | Butt joint, tongue-and-groove, cam-lock, or overlapping profile | Joint geometry varies by panel system and may include factory-formed seals or locking mechanisms. | Interlocking joints generally improve alignment and air tightness, while butt joints need more careful sealing and support. | Use tightly interlocking joints where hygiene, temperature control, or air leakage performance is important. |
| Joint sealing method | Compression gasket, sealant, tape, or combined sealing | Sealant and gasket selection should match the temperature range, substrate, moisture exposure, and movement. | Correct compression and continuous sealing reduce air and water leakage; contaminated or discontinuous joints can fail prematurely. | Prepare clean, dry contact surfaces and follow the joint manufacturer’s installation sequence. |
| Surface finish | Smooth, lightly embossed, or heavily profiled metal skin | The finish affects appearance, cleanability, scratch visibility, and contact with protective films or sealants. | Smooth surfaces are easier to clean and seal; profiled surfaces can conceal minor marks but require more care around trims and laps. | Select smooth finishes for hygienic interiors and controlled environments; use profiled finishes where appearance and impact resistance are priorities. |
| Coating and color | Pre-finished coated steel or other project-approved metal facings | Color and coating should be selected for UV exposure, corrosion conditions, cleaning chemicals, and design requirements. | Dark colors can absorb more solar heat, while damaged coatings may reduce corrosion protection; field cutting requires edge protection. | Use light colors in high-solar-load applications and specify coating performance according to the site environment. |
| Facing thickness | Light, standard, or heavy-gauge metal facings | Common metal skin thicknesses are approximately 0.4–0.8 mm, depending on design loads and system requirements. | Heavier facings improve resistance to handling damage and impact but increase panel weight and cutting effort. | Use stronger facings in high-traffic areas, exposed elevations, or locations requiring frequent cleaning. |
| Support and fastening | Steel or concrete supports with approved fasteners and washers | Fastener spacing depends on wind load, panel span, support strength, edge distance, and local building requirements. | Insufficient support or over-tightened fasteners can cause distortion, leakage, or damage to the panel skin. | Verify the structural fixing pattern before installation and keep fasteners aligned with the manufacturer’s guidance. |
| Fire and thermal requirements | Project-specific fire classification and U-value target | Performance depends on core density, panel assembly, facings, joints, and tested construction details. | Joints, penetrations, trims, and service openings must maintain the required continuity of the building envelope. | Confirm the complete tested assembly and local code requirements rather than selecting a panel by core material alone. |
| Site handling and cutting | Manual handling, lifting equipment, and controlled field cutting | Panel size and weight should match available labor, lifting equipment, access routes, and storage conditions. | Improper lifting, dragging, or abrasive cutting can deform edges, damage coatings, and compromise joint fit. | Store panels level and dry, lift them with suitable equipment, and protect finished faces during installation. |