| Aluminum melting temperature | Approximately 660.3 °C | Enables aluminum scrap to be processed at a lower temperature than ferrous metals, helping reduce thermal demand and furnace wear. | Actual operating temperatures are normally set above the melting point to support heat transfer, circulation, and complete melting. |
| Energy required for melting | Theoretical minimum: about 0.38 kWh/kg from 25 °C | Provides a useful benchmark for evaluating furnace efficiency and identifying heat losses. | Real energy consumption is higher because of furnace insulation, exhaust losses, scrap moisture, oxidation, holding time, and charging practices. |
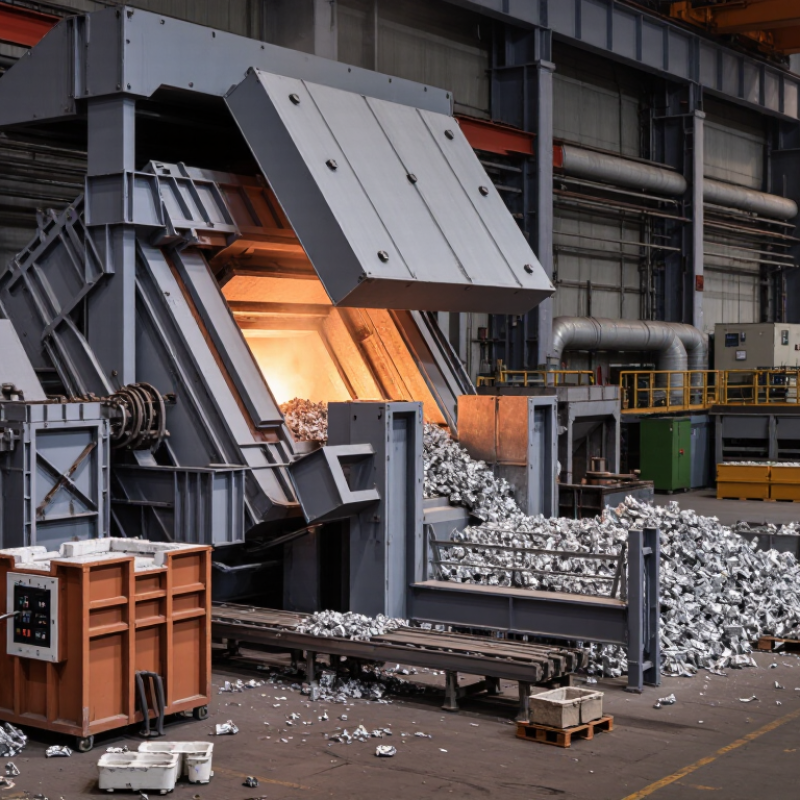
| Scrap volume reduction | Approximately 2.7 L of solid aluminum per kg | Converts bulky scrap into compact liquid metal, reducing storage space and simplifying downstream casting or alloy production. | The apparent volume reduction depends on scrap shape, packing density, coatings, attached materials, and dross formation. |
| Material recovery potential | High for clean, correctly sorted aluminum scrap | Allows valuable aluminum to be recovered repeatedly while reducing the need for primary aluminum production. | Recovery is affected by alloy mixing, oxidation, fines, paint, oil, moisture, furnace design, flux practice, and metal handling. |
| Typical charge materials | Castings, sheet, extrusion offcuts, turnings, and beverage cans | Supports flexible recycling of production returns and post-consumer scrap streams. | Turnings and lightweight scrap usually require controlled charging to limit oxidation and improve feeding safety. |
| Alloy flexibility | Suitable for many wrought and cast aluminum alloys | Enables recyclers to produce remelt ingots or molten metal for different applications. | Separate sorting and chemical analysis are important because copper, silicon, magnesium, iron, and zinc levels influence alloy quality. |
| Metal temperature control | Common process-control range: approximately 680–760 °C | Stable temperature control improves melt quality, pouring consistency, and production repeatability. | The appropriate temperature depends on alloy composition, casting method, holding time, and required fluidity. Excessive temperature can increase oxidation and hydrogen pickup. |
| Environmental advantage | Recycling aluminum generally uses far less energy than primary production | Reduces dependence on bauxite mining, alumina refining, and electrolytic aluminum production. | The total environmental benefit depends on electricity or fuel source, transport distance, scrap preparation, furnace efficiency, and emission controls. |
| Process integration | Melting, holding, skimming, alloy adjustment, and casting | A well-designed furnace system can combine several process stages, improving material flow and reducing repeated reheating. | Automation, temperature measurement, filtration, degassing, and dross management should be selected according to throughput and product requirements. |
| Key operating risks | Moisture explosions, oxidation, dross, fumes, and cross-contamination | Identifying risks helps improve operator safety, metal yield, and product consistency. | Scrap should be dry and inspected before charging; suitable ventilation, protective equipment, charging procedures, and emission controls are essential. |